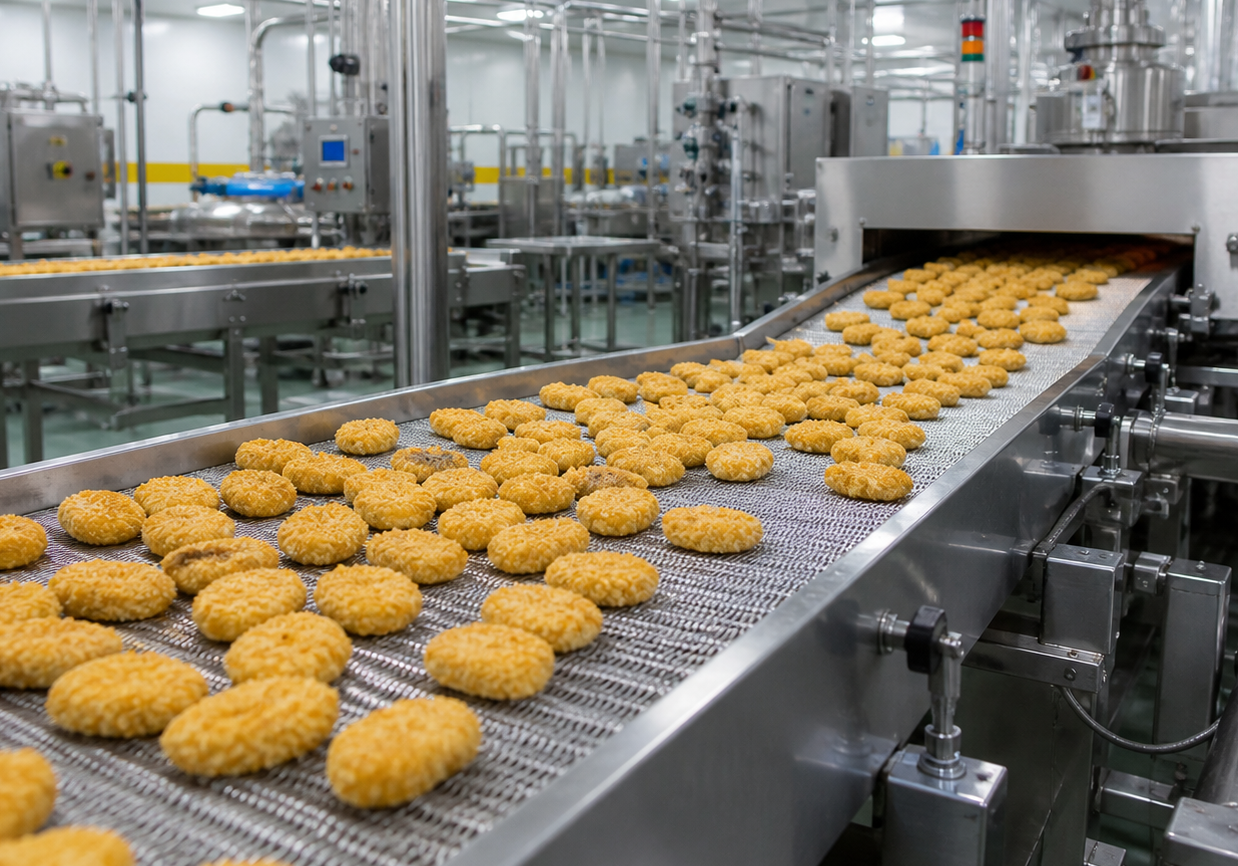

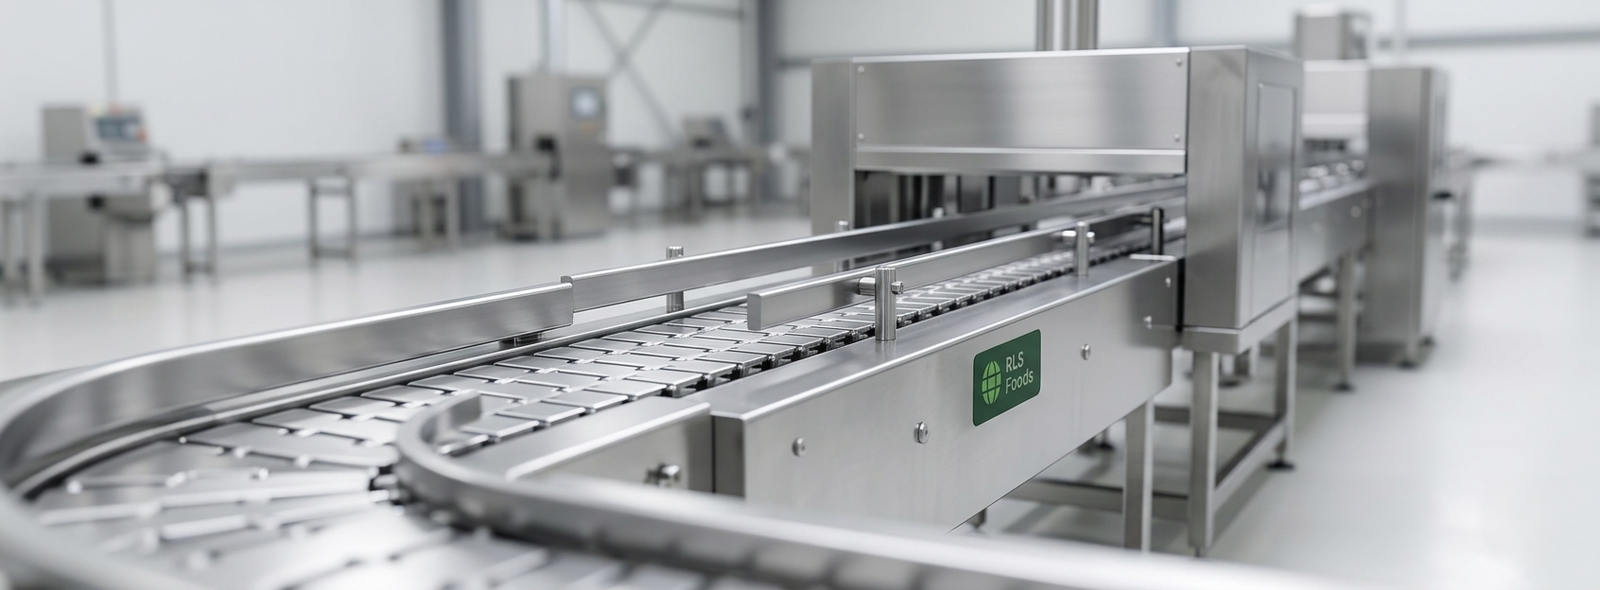
Modern Processing Unit
State-of-the-art frozen food manufacturing facility equipped with advanced machinery for efficient and hygienic food production.
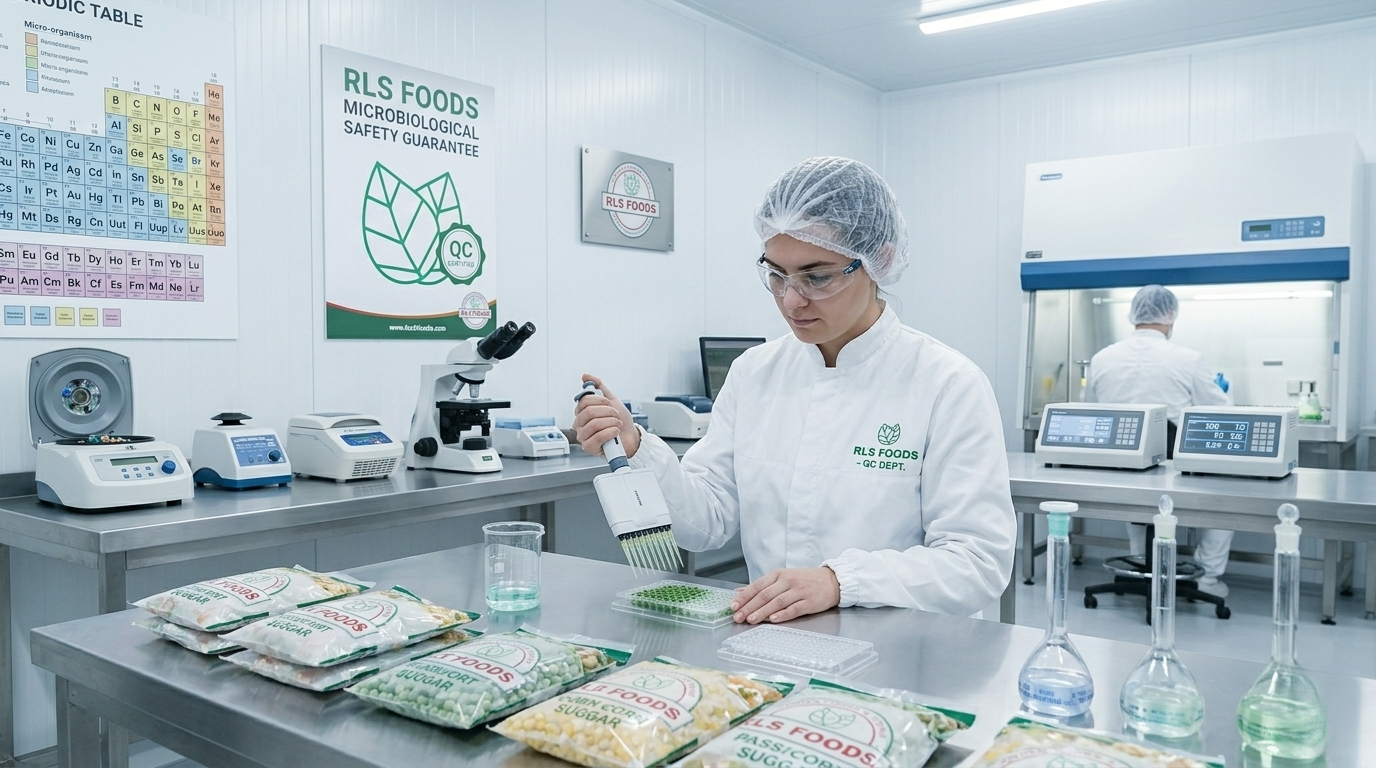
Quality Control Lab
Dedicated food quality testing laboratory ensuring safety, consistency and international compliance standards consistently.
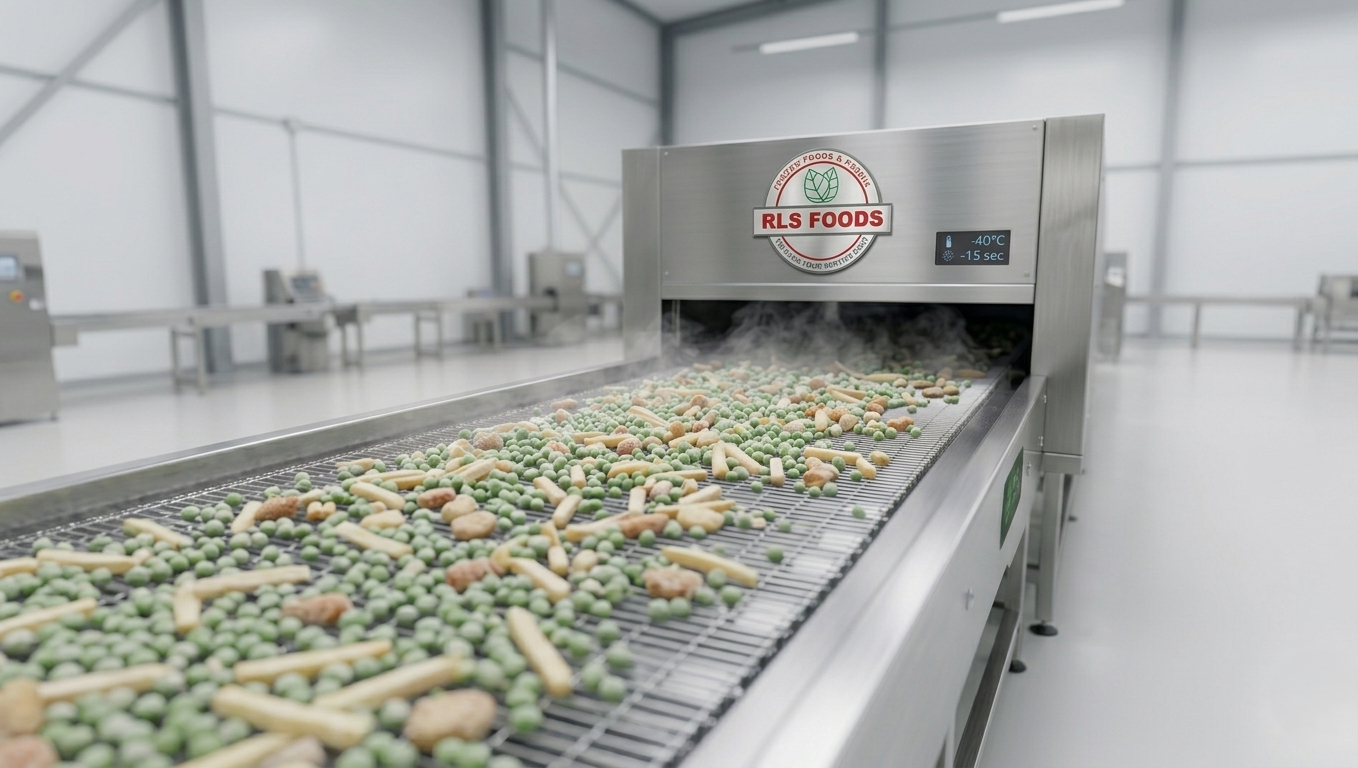
IQF & Freezing Technology
Advanced IQF freezing technology preserves freshness, texture and nutrition in every frozen food product.
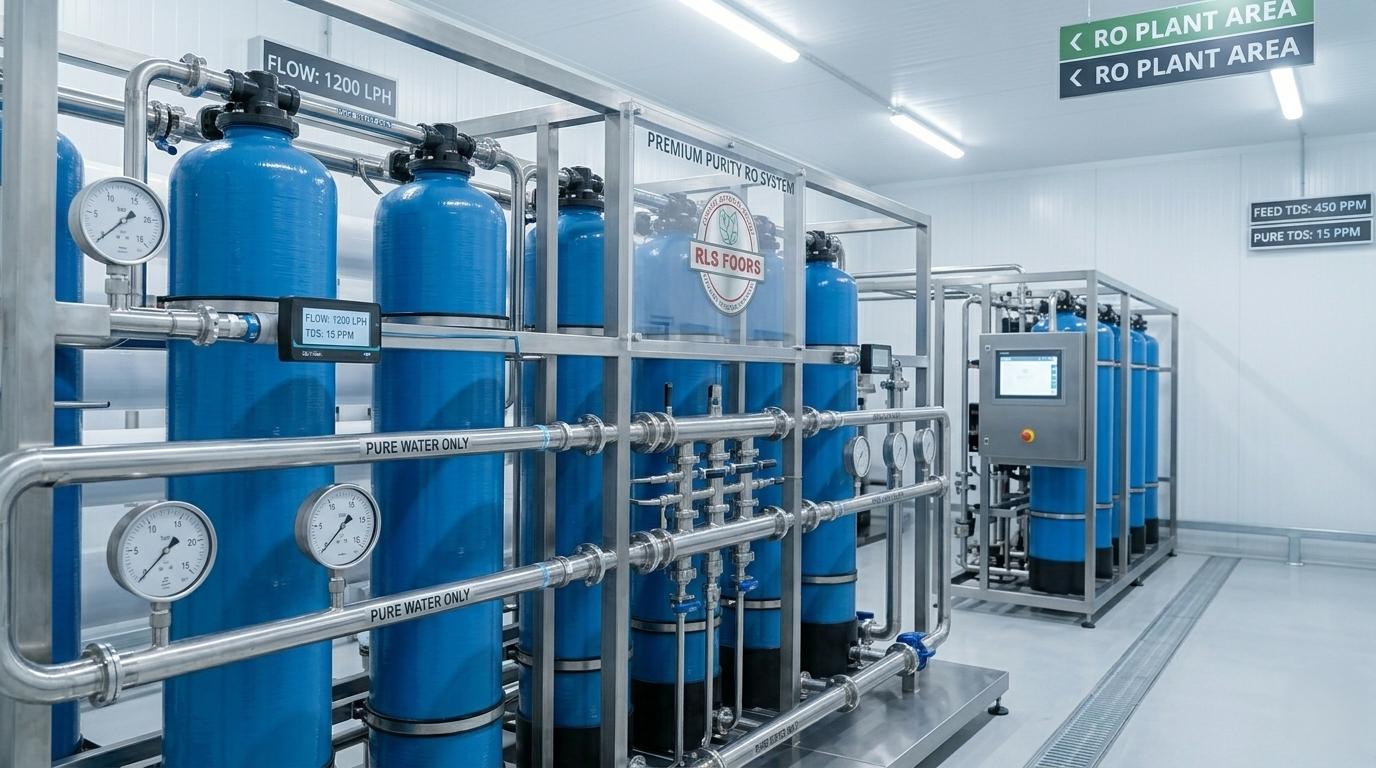
RO Water Treatment Plant
Advanced RO water purification system maintaining clean and safe water for food processing operations.
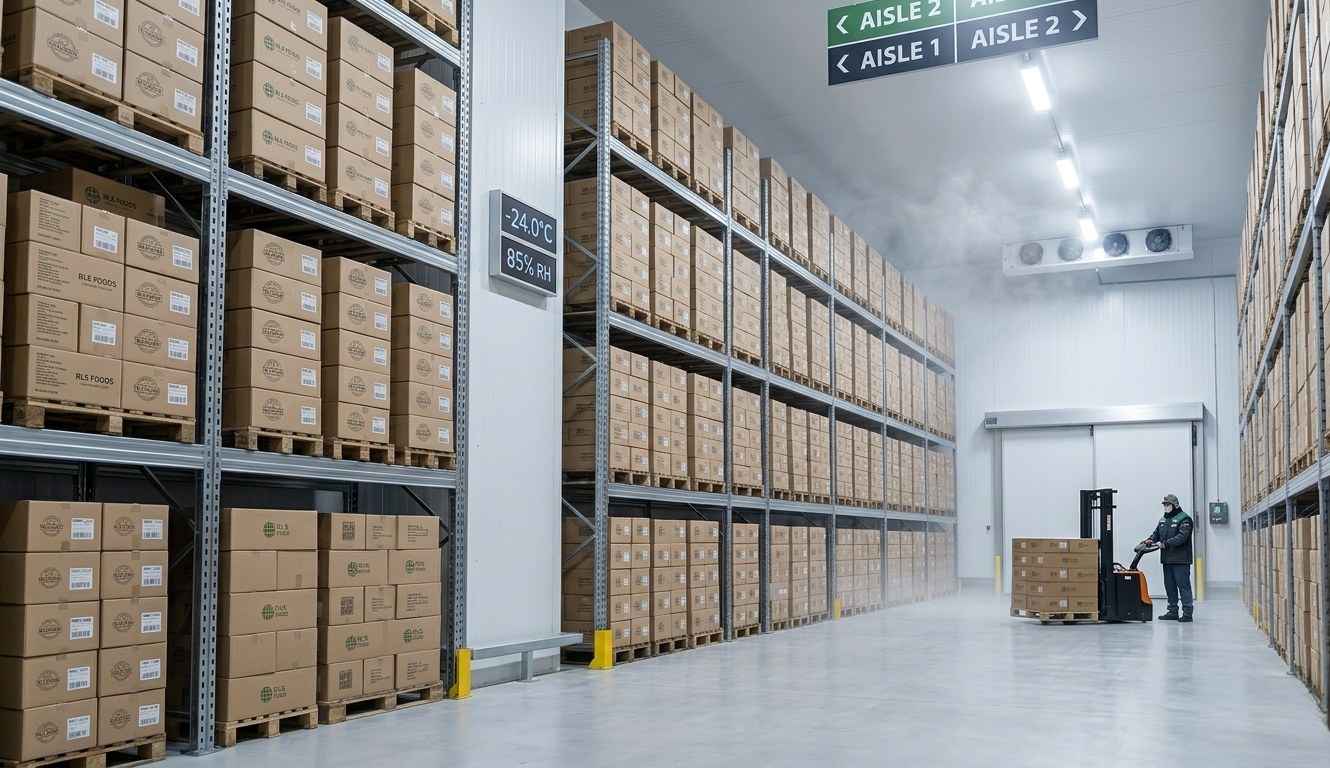
Cold Storage Facility
Large-scale cold storage infrastructure maintaining optimal temperature for frozen food safety and quality.
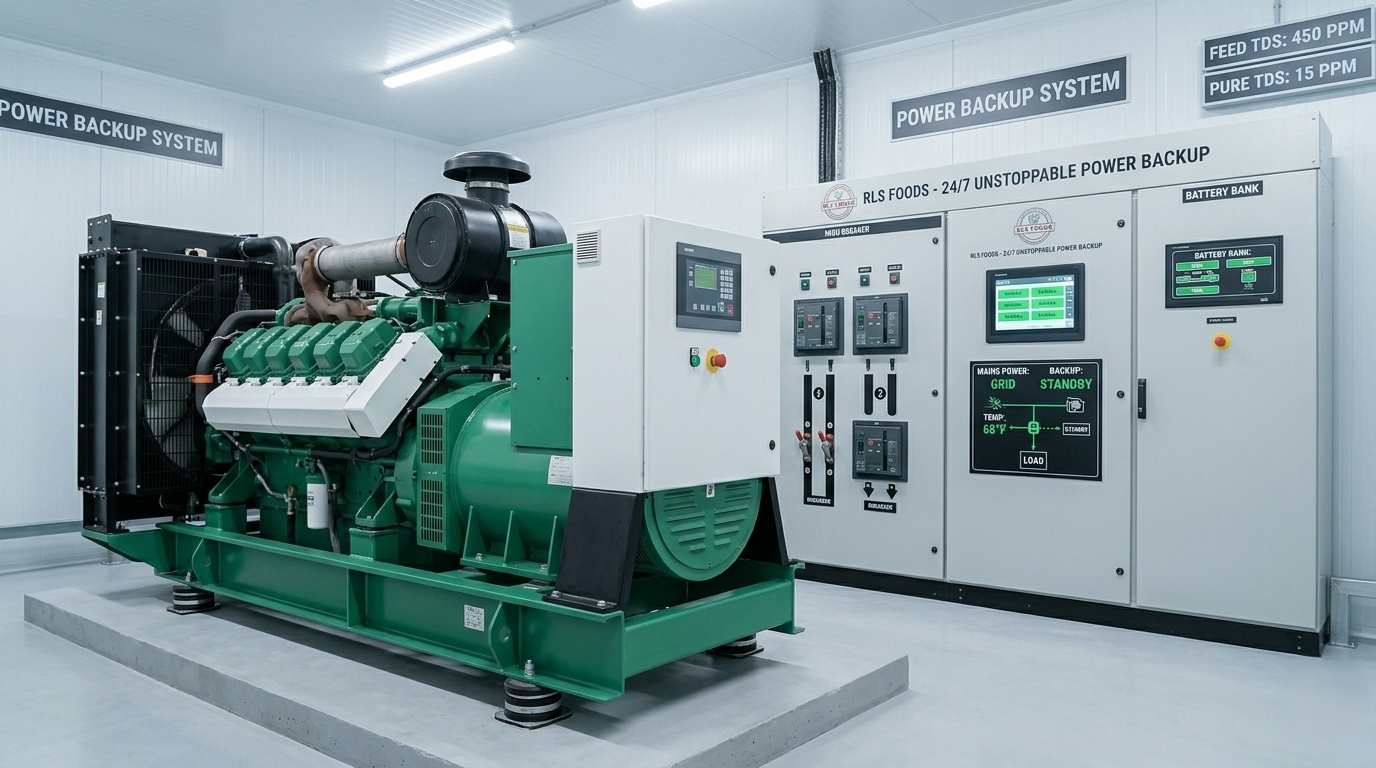
Power Backup
Reliable power backup system ensuring uninterrupted frozen food production and cold storage operations.
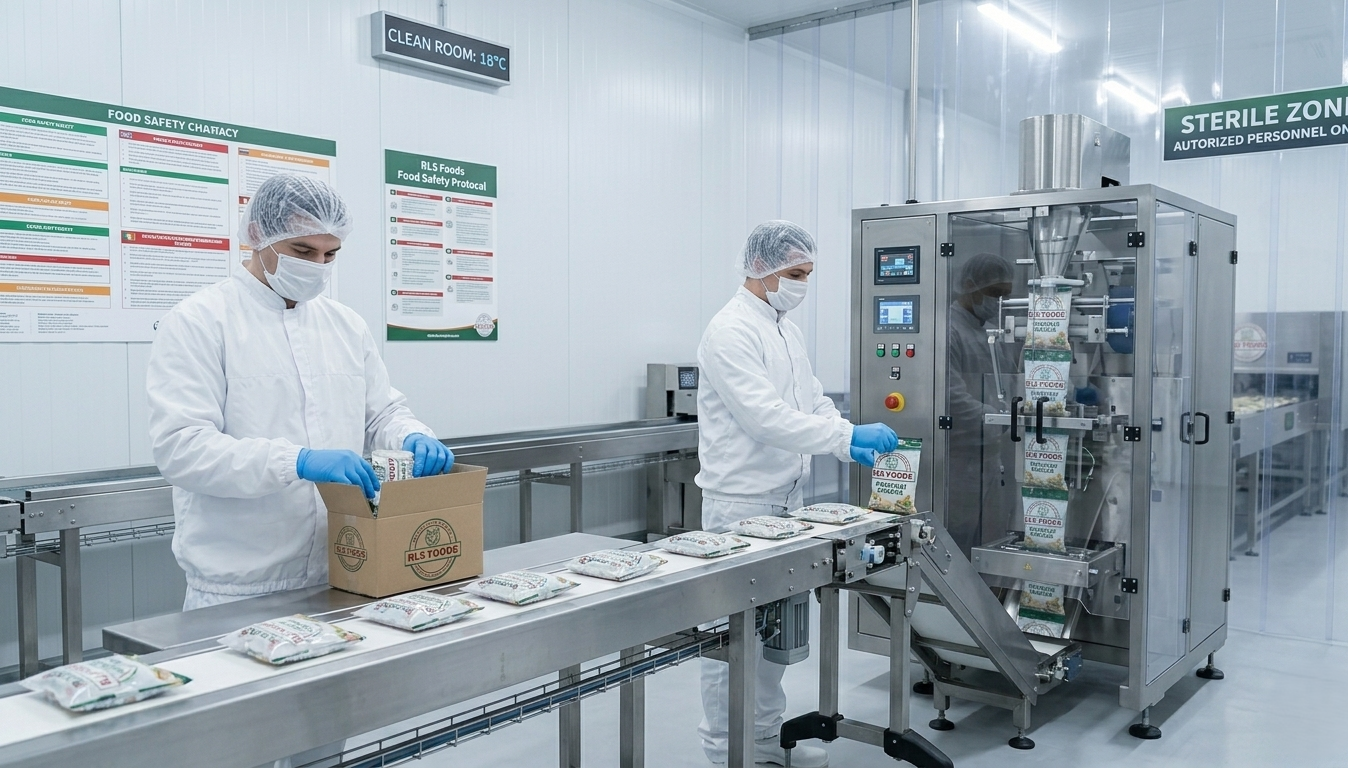
Hygienic Packaging
Premium food-grade export packaging designed to ensure freshness, hygiene and safe global transportation worldwide.
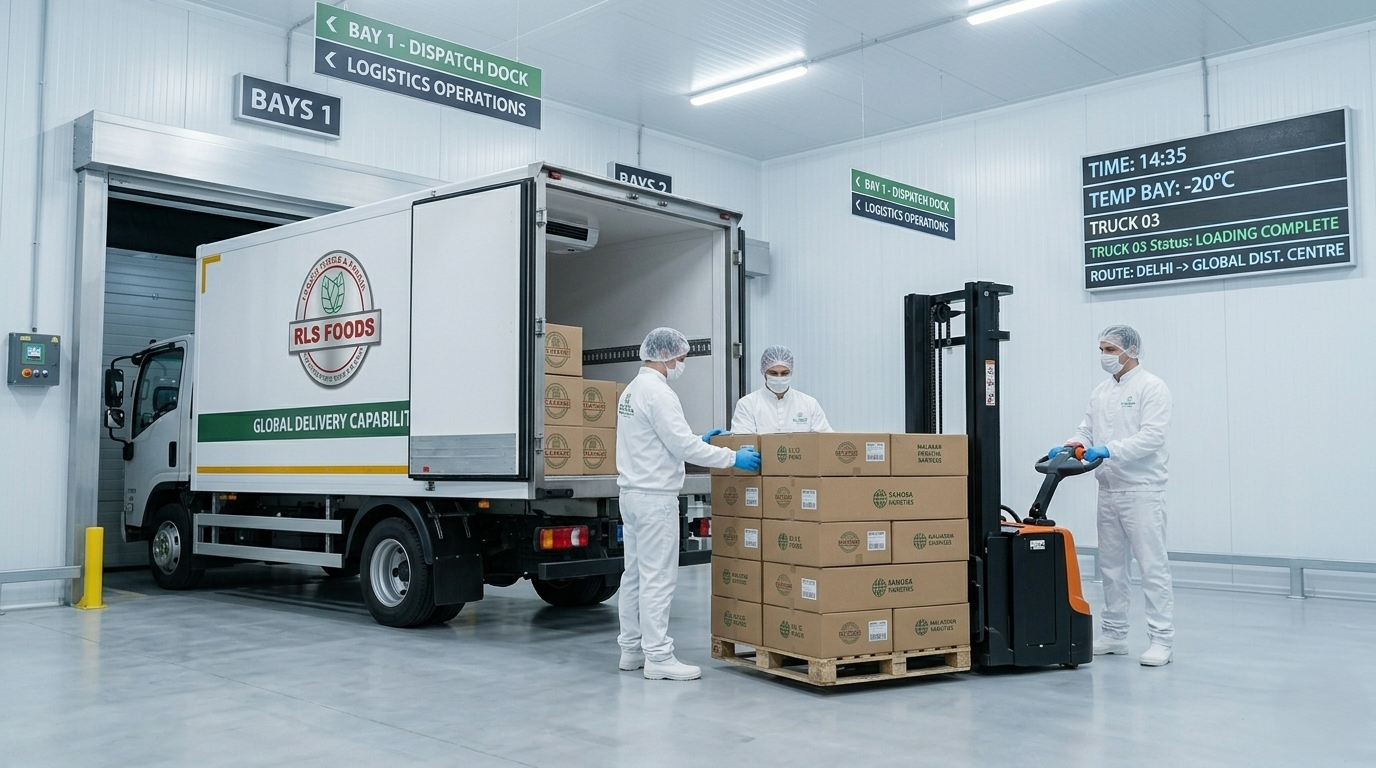
Efficient Logistics
Strong logistics network enabling smooth frozen food export and timely international delivery worldwide with reliable support.